At Rhodes Royce, we design and build complete turn-key biogas upgrading systems that transform raw methane from landfills, dairies, distilleries, and lagoons into clean, high-value Renewable Natural Gas (RNG). Our advanced process chain combines proven technologies for purification, compression, and control automation - guaranteeing 99% runtime, minimal maintenance and predictable performance for every installation. Here are the processes we have installed and commissioned at various RNG plants around the United States:
Moisture Removal (Dehydration) – eliminates water vapor to prevent corrosion and freezing in downstream equipment.
Particulate Filtration – removes dust, rust, and other solid contaminants.
Hydrogen Sulfide (H₂S) Removal – uses amine system with on site regeneration, activated carbon, or biological scrubbers to eliminate corrosive sulfur compounds.
Siloxane Removal – captures volatile silicon compounds that can damage engines and membranes.
Carbon Dioxide (CO₂) and Nitrogen Removal / Upgrading – increases methane purity through technologies such as:
Membrane Separation
Pressure Swing Adsorption (PSA)
Temperature Swing Adsorption (TSA)
Amine Processing
Cryogenic Separation
Compression – boosts gas pressure for processing, storage, or pipeline injection.
Oxygen Removal (Deoxygenation) – removes oxygen from biogas via a renewable and extremely effective catalyst process
Gas Cooling and Condensation – reduces temperature to separate condensate and enhance purification efficiency.
Gas Polishing / Final Filtration – ensures final gas purity and quality consistency.
Monitoring & Control Systems (SCADA / PLC) – provides real-time process automation, data logging, and remote performance optimization.
Odorization (Optional) – adds odorants before distribution to meet pipeline safety requirements.
Moisture Removal
Getting Biogas within pipeline specifications
H2S Removal
Siloxane Removal
Carbon Dioxide Removal (CO2)
Nitrogen Removal
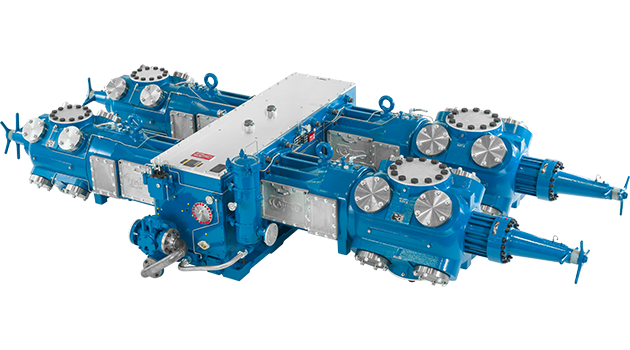
Biogas Compression