Rhodes Renewables stands on a foundation built over three generations of ingenuity, integrity, and hard work. What began in the oil and gas fields of the 1960s, with our grandfather’s pioneering spirit, has evolved into a modern leader in renewable gas processing and energy solutions. Today, our company is guided by a third-generation gas processor, supported by a family and network whose collective experience spans lifetimes in the industry. From field troubleshooting to full-scale plant design, our hands-on expertise ensures that every project is on schedule and exceeds the promises made. At Rhodes Renewables, there’s no problem we can’t solve—because our family has seen it all.
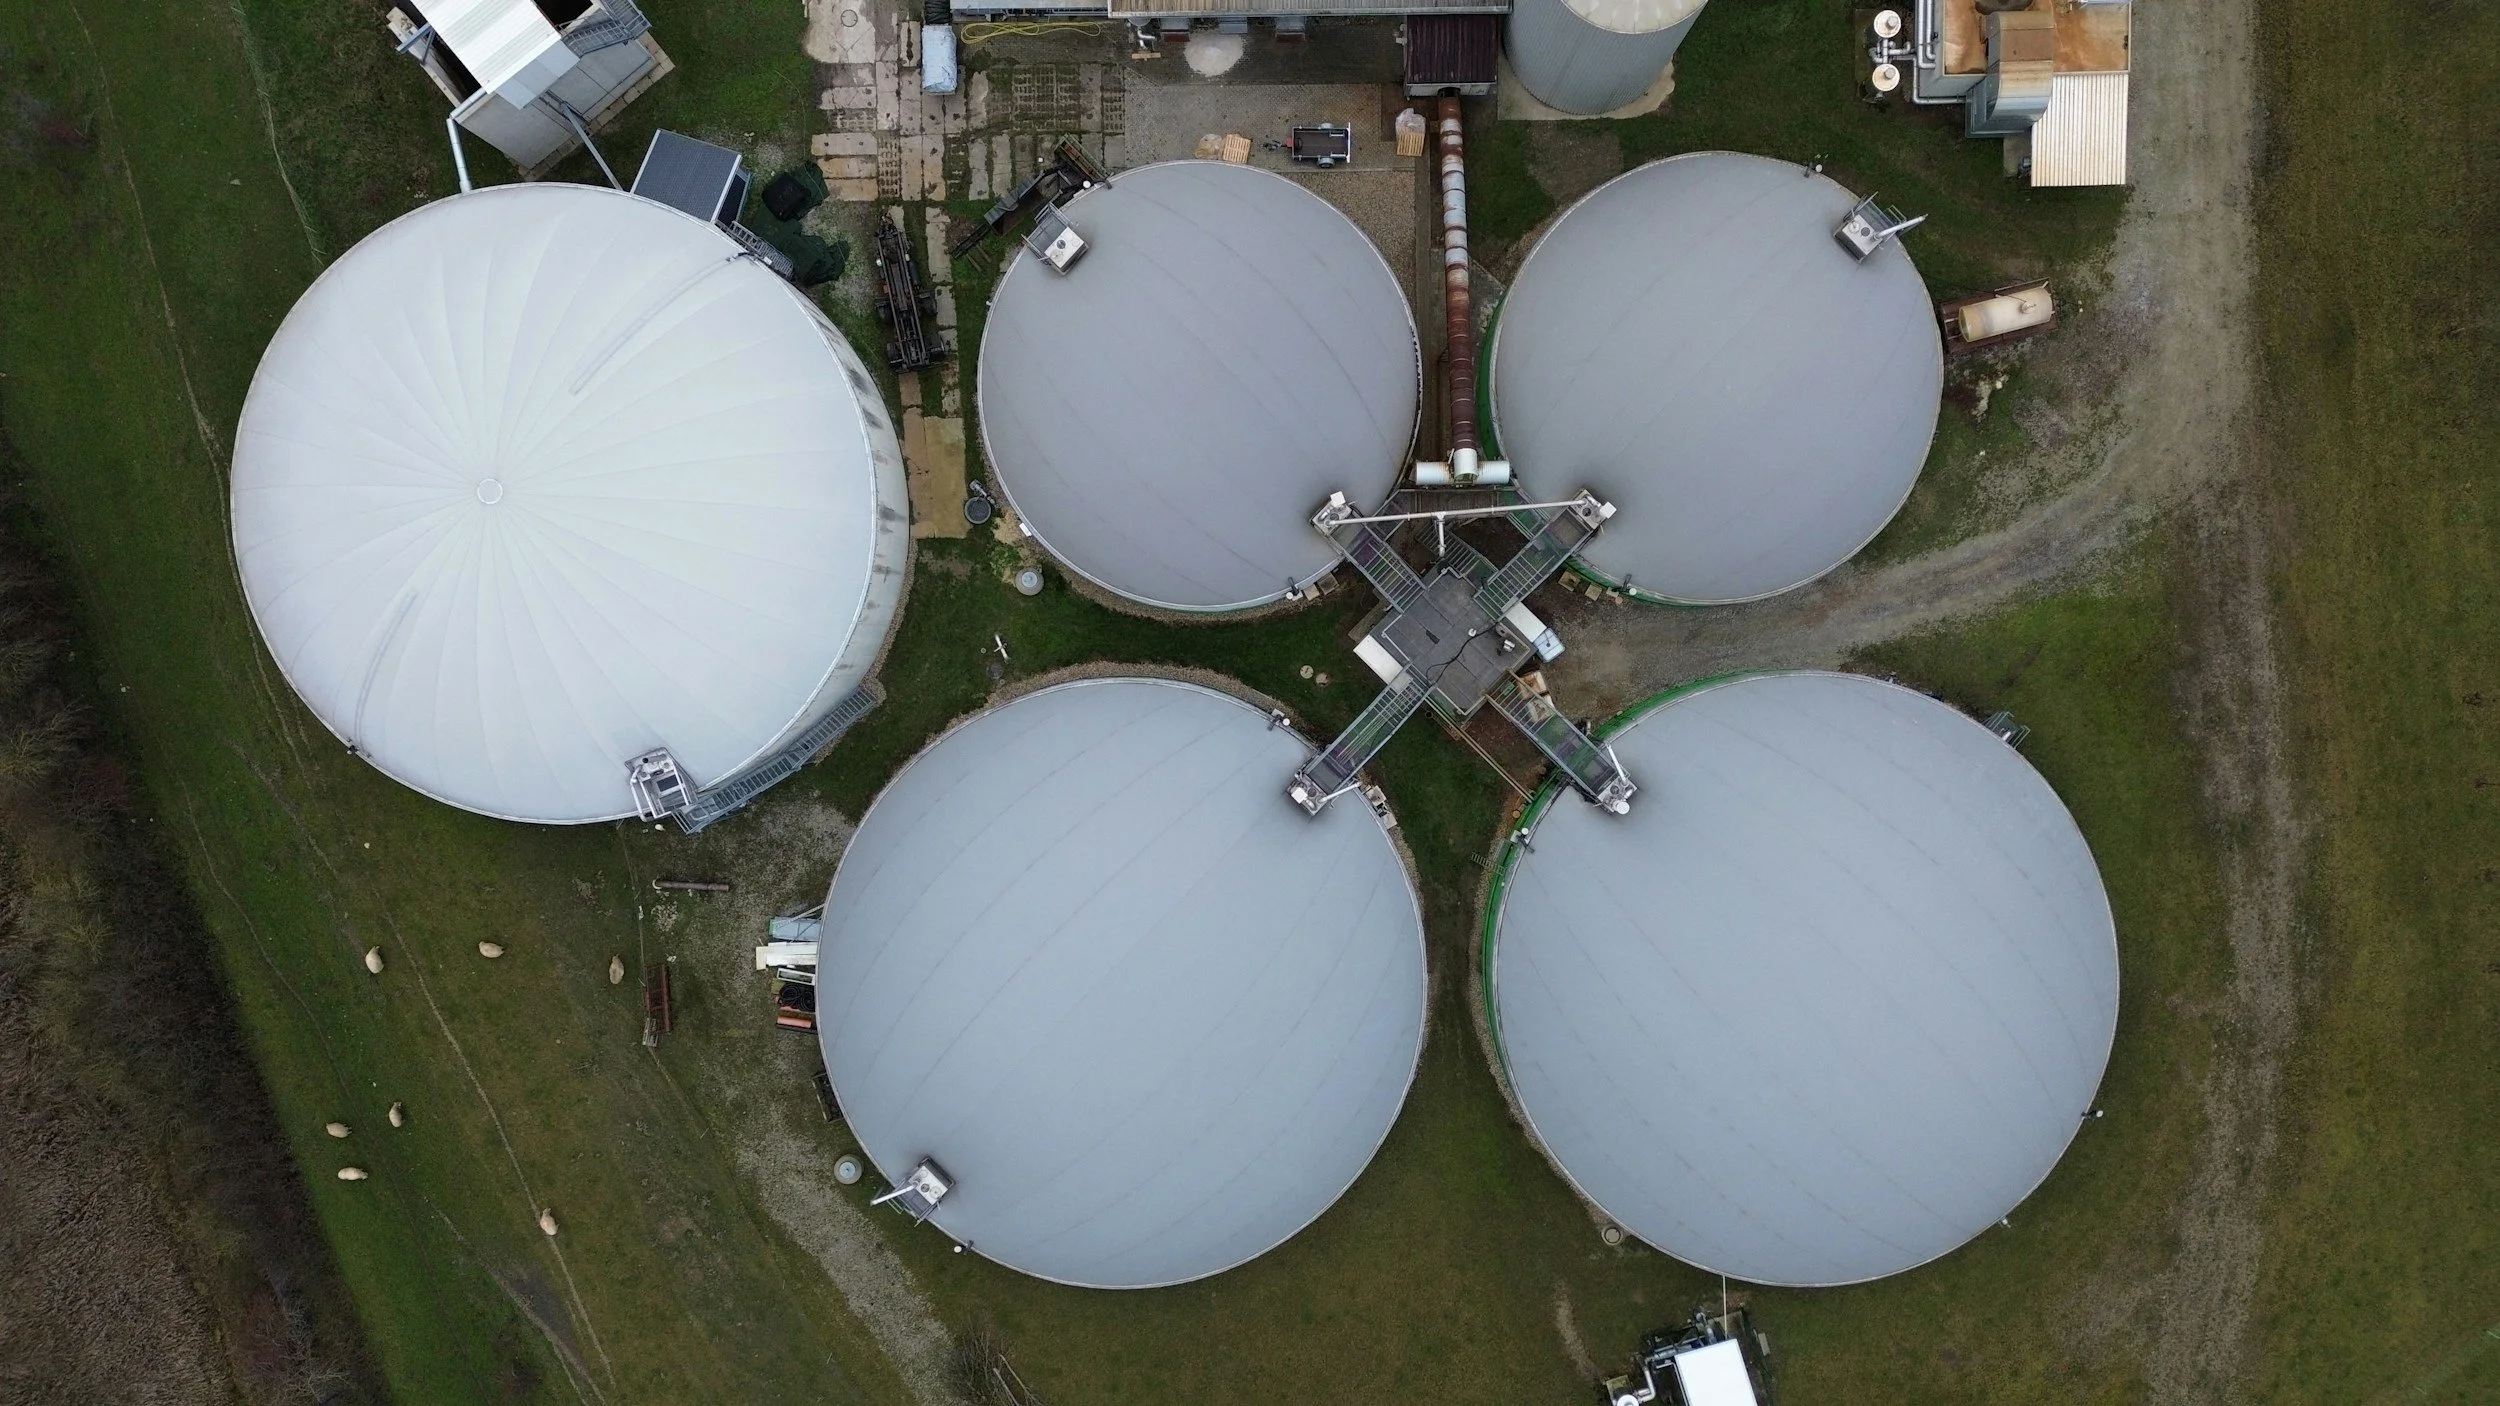
Rhodes Renewables designs and delivers complete turn-key biogas processing plant packages engineered for maximum reliability and efficiency. Each system is fully automated to ensure 99% uptime with minimal maintenance and operator interaction, while maintaining optimal gas quality and process stability. Our solutions integrate compression, purification, and monitoring technologies for landfills, dairies, distilleries, and lagoons, providing a seamless path from raw biogas to high-value renewable natural gas.
At Rhodes Renewables, we design and build complete turn-key biogas upgrading systems that transform raw methane from landfills, dairies, distilleries, and lagoons into clean, high-value Renewable Natural Gas (RNG). Our advanced process chain combines proven technologies for purification, compression, and control automation - delivering 99% runtime, minimal maintenance and predictable performance for every installation. Here are the processes we have installed at various RNG plants around the United States:
Moisture Removal (Dehydration) – eliminates water vapor to prevent corrosion and freezing in downstream equipment.
Particulate Filtration – removes dust, rust, and other solid contaminants.
Hydrogen Sulfide (H₂S) Removal – uses iron sponge, activated carbon, or biological scrubbers to eliminate corrosive sulfur compounds.
Siloxane Removal – captures volatile silicon compounds that can damage engines and membranes.
Carbon Dioxide (CO₂) and Nitrogen Removal / Upgrading – increases methane purity through technologies such as:
Membrane Separation
Pressure Swing Adsorption (PSA)
Temperature Swing Adsorption (TSA)
Amine Processing
Cryogenic Separation
Compression – boosts gas pressure for processing, storage, or pipeline injection.
Oxygen Removal (Deoxygenation) – removes oxygen from biogas via a renewable and extremely effective catalyst process
Gas Cooling and Condensation – reduces temperature to separate condensate and enhance purification efficiency.
Gas Polishing / Final Filtration – ensures final gas purity and quality consistency.
Monitoring & Control Systems (SCADA / PLC) – provides real-time process automation, data logging, and remote performance optimization.
Odorization (Optional) – adds odorants before distribution to meet pipeline safety requirements.